
Offcanvas top
Elbow Pipe Fittings Types and Applications | FW Trading
Elbow Pipe Fittings Types and Applications: The Complete Piping Engineer’s Guide for Dubai & UAE
Selecting the wrong elbow is rarely a purchasing error alone. It shows up later as erosion at a bend, a failed hydrotest, or a weld that cannot be inspected. This guide covers elbow pipe fittings types and applications for engineers, MEP contractors, and procurement teams working across Dubai, the UAE, and the GCC.
You will find angle and radius selection logic, connection standards, material grades, and sector-specific use cases. A decision matrix and pre-order checklist at the end help you specify elbows correctly the first time.
Table of Contents
- What Are Elbow Pipe Fittings and Why Does Selection Matter?
- How Are Elbow Pipe Fittings Classified by Angle?
- Long Radius vs Short Radius Elbow: Which Is Better?
- Which Elbow End Connections and Standards Apply?
- Which Material Is Best for Elbow Pipe Fittings in the UAE?
- Which Elbow Pipe Fittings Types and Applications Suit Dubai Industries?
- How Do You Specify an Elbow Correctly?
- What Should You Remember When Choosing Elbow Pipe Fittings?
- Frequently Asked Questions
What Are Elbow Pipe Fittings and Why Does Selection Matter?
An elbow pipe fitting is a curved component that changes flow direction in a piping system, typically by 45, 90, or 180 degrees. Selection matters because every elbow adds pressure drop, concentrates erosion and stress, and must match the pipe’s schedule, material, and code rating.
Elbows are the most numerous fitting in most process lines, and they are where problems concentrate. Three failure vectors dominate field inspections: erosion on the outer wall of the bend, wall thinning at the extrados, and bore mismatch at the weld joint.
When sourcing industrial elbow pipe fittings in Dubai, the recurring problem is an incomplete order. Angle and size are stated, but schedule, radius, or grade are missing. Each gap forces an assumption that surfaces later at inspection.
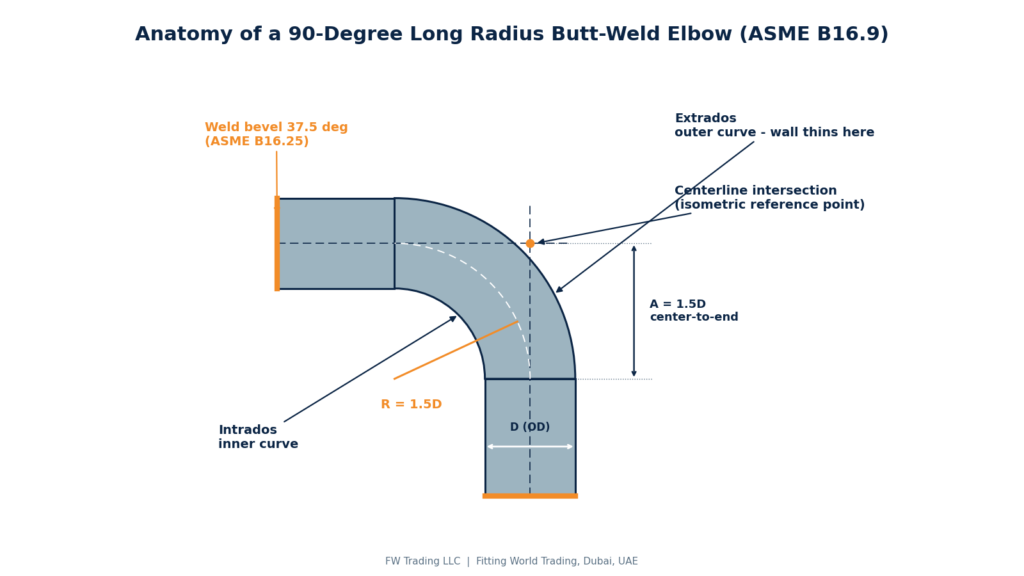
Four terms appear on every elbow drawing:
- Intrados: the inner curve of the bend.
- Extrados: the outer curve, where wall thinning occurs during forming.
- Center-to-end: the dimension used on isometrics to locate the fitting.
- Bevel: the weld-end preparation, typically 37.5° per ASME B16.25.
How Are Elbow Pipe Fittings Classified by Angle?
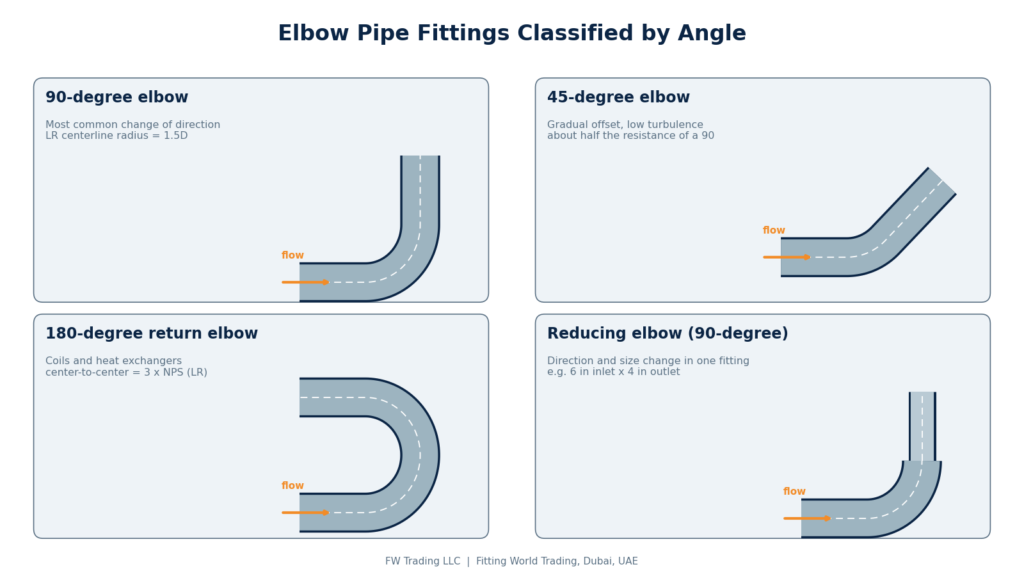
Elbows are classified by turning angle: 90-degree elbows redirect flow perpendicularly, 45-degree elbows create gradual offsets, 180-degree return bends reverse flow, and reducing elbows combine a direction change with a size change. Each angle carries a different pressure-drop penalty and layout footprint.
What Is a 90-Degree Elbow Used For?
A 90-degree elbow turns flow through a right angle and is the most widely specified elbow in industrial piping. It is used wherever a line must change plane, such as at pump discharges, pipe rack turns, and equipment nozzles, and it is available in long radius and short radius forms.
Because the flow is forced through a full right-angle turn, the outer wall takes the highest impact load. For slurry, wet steam, or sand-laden produced water, specify long radius with a heavier schedule, or use a 3D or 5D bend.
When Should You Choose a 45-Degree Elbow?
Choose a 45-degree elbow when you need a gradual change of direction or a pipe offset with minimal turbulence. It contributes roughly half the resistance of a 90-degree elbow, which makes it suitable for steam, compressed air, hydraulic, and drainage lines where pressure drop and water hammer must stay low.
A pair of 45-degree elbows separated by a short spool often gives a smoother path than a single short radius 90-degree elbow. The tradeoff is extra welds, extra inspection, and a longer layout. The table below compares the two.
| Parameter | 90-degree elbow | 45-degree elbow |
|---|---|---|
| Direction change | 90° | 45° |
| Relative resistance | Higher | Roughly 50% of a 90° |
| Erosion at outer wall | Highest | Lower |
| Fittings needed for a 90° turn | 1 | 2 |
| Layout footprint | Compact | Longer |
| Typical use | Pump discharge, rack turns | Offsets, steam, compressed air, drainage |
Where Are 180-Degree Return Elbows Used?
A 180-degree return elbow reverses flow direction through a U-shaped turn with a fixed center-to-center spacing. It is used in heating coils, heat exchanger piping, fired heater coils, and compact serpentine runs where fluid must double back without a long straight section.
Under ASME B16.9, long radius returns have a center-to-center spacing of three times the nominal pipe size, and short radius returns use two times. Confirm the spacing before routing coils, because it fixes the pitch of the run.
What Is a Reducing Elbow?
A reducing elbow changes both the direction and the pipe diameter in one fitting, for example a 90-degree elbow with a 6-inch inlet and a 4-inch outlet. It saves a weld and reduces fitting count, but availability is limited, so many projects specify an elbow plus a concentric reducer instead.
Where the required combination is not stocked, specify a standard elbow with a concentric reducer. Confirm that the reducer’s schedule matches the downstream pipe.
Long Radius vs Short Radius Elbow: Which Is Better?
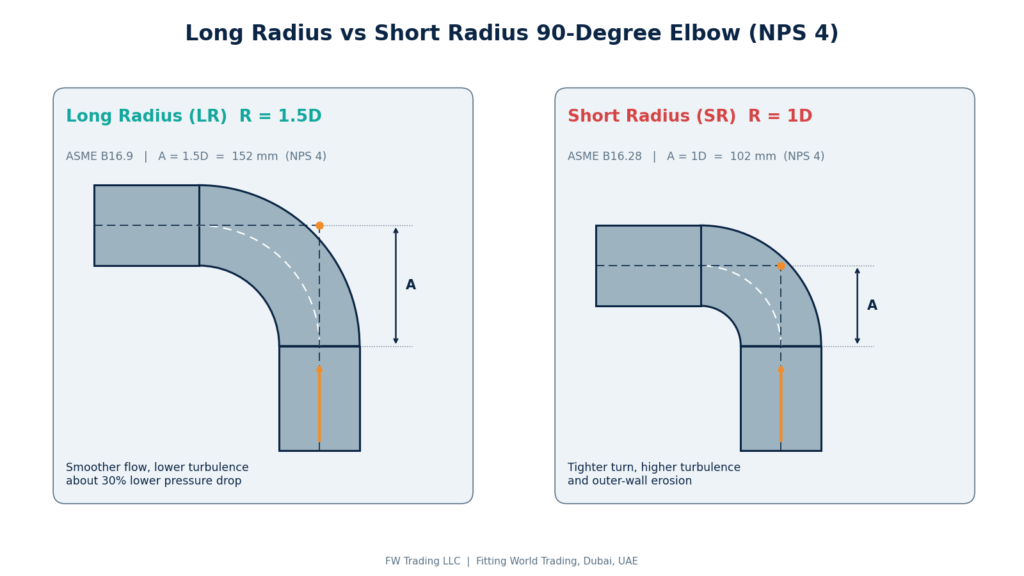
A long radius (LR) elbow has a bend radius of 1.5 times the nominal pipe diameter, while a short radius (SR) elbow has a radius of 1 times the diameter. LR elbows reduce pressure drop and erosion, so they are the default choice. SR elbows are used only where space is restricted.
| Parameter | Long radius (LR) | Short radius (SR) |
|---|---|---|
| Bend radius | 1.5D | 1D |
| Governing standard | ASME B16.9 | ASME B16.28 |
| Center-to-end, NPS 4, 90° | 152 mm | 102 mm |
| Resistance coefficient (K) | About 14 fT | About 20 fT |
| Erosion at bend | Lower | Higher |
| Space required | More | Less |
| Typical use | Process, oil and gas, steam, high flow | Tight skids, low-flow retrofit |
fT is the friction factor in fully turbulent flow. Confirm K values in your project hydraulic design basis.
How Does Elbow Radius Affect Pressure Drop and Velocity?
A longer radius reduces the abruptness of the turn, which lowers the resistance coefficient and the local turbulence. A long radius elbow typically produces roughly 30% lower pressure drop than a short radius elbow at the same flow, and it also reduces erosive wear when velocity approaches the erosional limit.
Crane TP-410 lists roughly 20 fT at r/d = 1 and 14 fT at r/d = 1.5 for 90-degree bends. That gap compounds across a line with dozens of turns.
For oil and gas service, check the erosional velocity limit in API RP 14E: Ve = C / √ρ, with C = 100 for continuous service, ρ in lb/ft³, and Ve in ft/s.
When Is a Short Radius Elbow the Right Choice?
A short radius elbow is the right choice when space is limited and flow is low, such as compact skids, tight pipe racks, and retrofit work around existing equipment. SR elbows follow ASME B16.28 and save up to one-third of the bend footprint, but should not be used in erosive or high-velocity service.
Apply these decision rules:
- Default to LR unless a documented layout constraint prevents it.
- Avoid SR on slurry, wet steam, and any line near its erosional velocity.
- Check that 1D center-to-end leaves weld and inspection access.
- Record any LR/SR mix in the piping class so procurement does not substitute.
Which Elbow End Connections and Standards Apply?
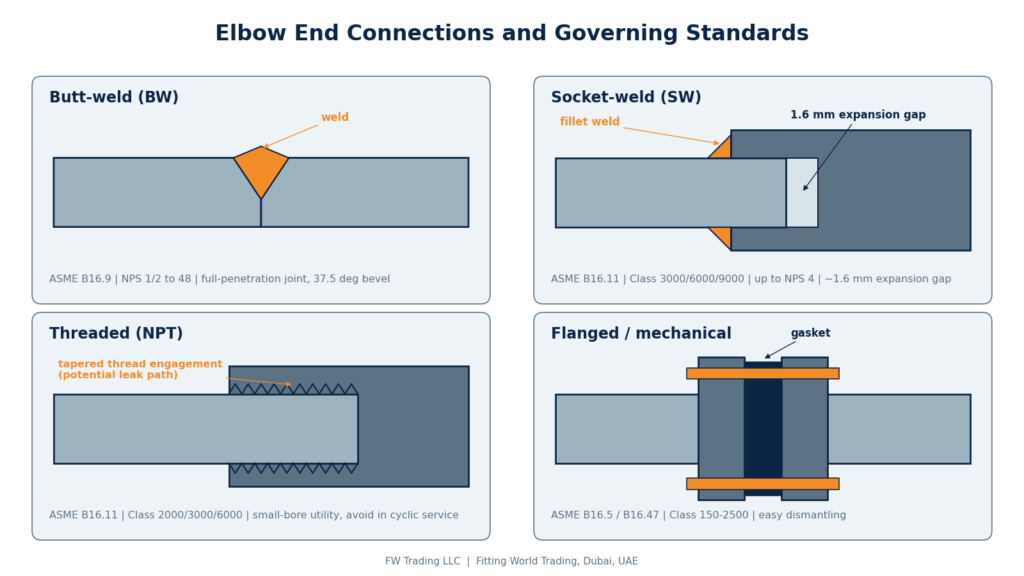
Elbow end connections determine the joining method and governing standard. Butt-weld elbows follow ASME B16.9 for large-bore, high-pressure process lines, socket-weld and threaded elbows follow ASME B16.11 for small-bore piping, and flanged or mechanical ends suit equipment that needs frequent dismantling.
What Are Butt-Weld Elbows (ASME B16.9)?
Butt-weld (BW) elbows are welded directly to the pipe end after a bevel preparation, creating a continuous, full-penetration joint. Manufactured to ASME B16.9, they suit NPS 1/2 to 48 process, oil and gas, and steam lines where leak-tightness, fatigue resistance, and radiographic inspection are required.
Key points for BW elbows:
- Match the elbow wall to the pipe schedule (STD, XS, SCH 40, 80, 160) to avoid internal mismatch that disturbs flow and complicates radiography.
- Verify the 37.5° bevel and root face per ASME B16.25 before fit-up.
- Design under ASME B31.3 (process), B31.1 (power), or B31.4 and B31.8 (pipelines).
Our guide on factors to consider when choosing buttweld fittings covers wall thickness and end preparation. Always confirm the elbow matches your carbon and stainless steel pipes in schedule and grade.
Where Do Socket-Weld and Threaded Elbows Fit?
Socket-weld (SW) and threaded (NPT) elbows are forged steel fittings under ASME B16.11 for small-bore pipe, typically NPS 2 and below. Socket-weld fittings are rated Class 3000, 6000, or 9000, and threaded fittings are rated Class 2000, 3000, or 6000. They suit instrument, utility, and high-pressure small lines.
- Socket-weld: leave a gap of about 1.6 mm (1/16 in) between the pipe end and the socket shoulder before welding, to avoid cracking from thermal expansion.
- Threaded: every thread is a potential leak path and crevice. Avoid threaded joints in cyclic, vibrating, or hazardous service.
- Sourcing: review our threaded fittings and high pressure fittings for forged small-bore options.
Why Choose Flanged and Mechanical Elbows?
Flanged and mechanical-joint elbows let crews dismantle a line without cutting or hot work. Flanged elbows bolt to mating flanges with a gasket and fasteners matched to the pressure class, while grooved and mechanical couplings join plain-end or grooved-end elbows in minutes. They suit pump skids, HVAC plant rooms, and maintenance-heavy equipment.
Pair flanged elbows with correctly rated industrial flanges and compatible flange gaskets. Our guide on choosing the right flange explains type, face, and rating.
| Connection | Standard | Rating basis | Typical sizes | Best for |
|---|---|---|---|---|
| Butt-weld | ASME B16.9 / B16.28 | Schedule (STD, XS, 40, 80, 160) | NPS 1/2 to 48 | High-pressure process, steam, oil and gas |
| Socket-weld | ASME B16.11 | Class 3000 / 6000 / 9000 | Up to NPS 4 | Small-bore, high-pressure, instrument lines |
| Threaded (NPT) | ASME B16.11 | Class 2000 / 3000 / 6000 | Up to NPS 4 | Utility, low-risk small-bore |
| Flanged | ASME B16.5 / B16.47 | Class 150 to 2500 | NPS 1/2 and up | Equipment connections, maintenance access |
Planning a material take-off? Download the FW Trading product catalog to check available sizes, schedules, and grades before you finalize your line list.
Which Material Is Best for Elbow Pipe Fittings in the UAE?
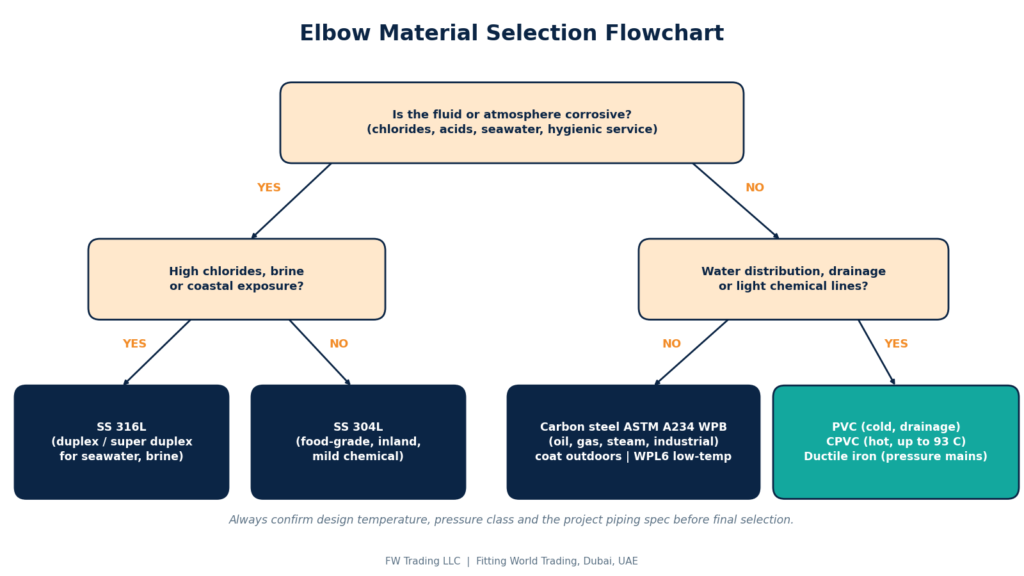
Match material to fluid, temperature, and environment. Use ASTM A234 WPB carbon steel for oil, gas, and steam, SS 304/304L or 316/316L stainless steel for corrosive, coastal, and food-grade service, and PVC, CPVC, or ductile iron for water distribution and drainage.
When Should You Specify Carbon Steel ASTM A234 WPB?
Specify ASTM A234 WPB for high-stress oil, gas, and industrial steam piping at approximately -29°C to 400°C where the fluid is not corrosive. It is the standard carbon steel elbow grade, but it needs coating or cathodic protection in humid, salt-laden coastal conditions.
In Dubai’s climate, external corrosion often limits service life more than the process fluid. Specify epoxy or polyurethane coating systems for outdoor lines. For low-temperature service, ASTM A420 WPL6 replaces WPB.
When Is Stainless Steel Mandatory?
Stainless steel elbows are mandatory when the fluid or atmosphere would corrode carbon steel, including chlorides, acids, seawater, and hygienic process lines. Grades 304/304L suit general corrosive and food-grade service, while 316/316L adds molybdenum for superior chloride and pitting resistance in coastal UAE projects and chemical plants.
Both grades are supplied to ASTM A403 as WP304/304L and WP316/316L. The L grades cap carbon at 0.03% to resist sensitization during welding. Request PMI testing and EN 10204 3.1 certificates to verify grade on receipt.
For stock availability, see our range of stainless steel pipe elbows UAE projects specify most often.
Where Do PVC, CPVC and Ductile Iron Elbows Fit?
PVC, CPVC, and ductile iron elbows serve municipal water distribution, drainage, and light chemical lines. PVC suits cold water and drainage, CPVC handles hotter water and mild chemicals up to about 93°C, and ductile iron elbows with mechanical joints carry high-pressure potable and fire water mains.
PVC elbows follow ASTM D2466 (SCH 40) and CPVC follows ASTM F439 (SCH 80). Derate PVC pressure ratings above 23°C. Ductile iron fittings follow AWWA C110 and C153 and need cement-mortar or epoxy lining.
| Material | Standard | Typical service | Limitation |
|---|---|---|---|
| Carbon steel | ASTM A234 WPB | Oil, gas, steam, industrial lines | Needs coating in coastal air |
| Stainless 304/304L | ASTM A403 WP304/304L | Food-grade, general corrosive | Pitting in high chlorides |
| Stainless 316/316L | ASTM A403 WP316/316L | Coastal MEP, chemical, desalination | Higher cost |
| PVC | ASTM D2466 | Cold water, drainage | Pressure derates with heat |
| CPVC | ASTM F439 | Hot water, mild chemicals | Limited to about 93°C |
| Ductile iron | AWWA C110 / C153 | Municipal water, fire mains | Weight, lining required |
Which Elbow Pipe Fittings Types and Applications Suit Dubai Industries?
Elbows appear in every UAE piping sector, but the specification differs. Refineries and upstream oil and gas use butt-weld carbon steel LR elbows, desalination and coastal MEP use 316L or duplex, HVAC uses carbon steel or copper, and power plants use alloy elbows for high-temperature steam.
Oil and Gas and Refineries
Use LR butt-weld elbows in ASTM A234 WPB, SCH 40 to 160, designed to ASME B31.3 or B31.4/B31.8. Sour service under NACE MR0175/ISO 15156 requires hardness control. Use A420 WPL6 where low design temperatures apply.
Desalination and Water Treatment
Brine and seawater lines call for 316L, duplex, or super duplex stainless steel. Low-pressure intake and chemical dosing lines use PVC, CPVC, or GRP. Pair elbows with corrosion-rated marine valves and gaskets.
Power Generation
High-temperature steam uses alloy steel elbows such as ASTM A234 WP11 or WP22 under ASME B31.1. Feedwater and condensate lines typically use WPB. Long radius is standard to limit erosion.
HVAC, Fire Protection and Plumbing
Chilled water and district cooling plant rooms use carbon steel SCH 40 with flanged or grooved joints for maintenance access. Small-bore drains and instrument lines use SW or threaded elbows. CPVC serves hot and cold domestic water. Fire protection elbows must be listed and installed per the UAE Fire and Life Safety Code.
Commercial Construction
High-rise and mixed-use projects combine all of the above in one building: ductile iron or PVC for drainage and risers, carbon steel for HVAC, stainless steel for potable and hygienic lines. Keep a single material schedule per system to avoid substitution at site.
How Do You Specify an Elbow Correctly?
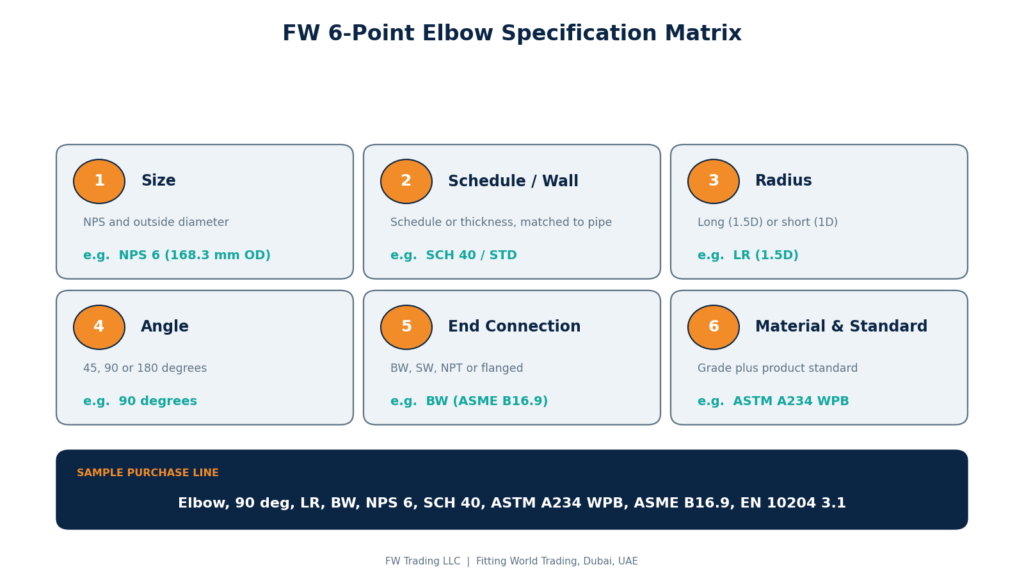
Specify an elbow with six parameters: size (NPS), schedule or wall thickness, radius (LR or SR), angle, end connection, and material grade with standard. Missing any one of these parameters invites a mismatch at fabrication, delays at the site, or a rejected material receipt. Add the applicable code and certificate type.
The FW 6-Point Elbow Specification Matrix keeps purchase orders unambiguous:
| # | Parameter | What to state | Example |
|---|---|---|---|
| 1 | Size | NPS and OD | NPS 6 (168.3 mm OD) |
| 2 | Schedule / wall | Schedule or thickness | SCH 40 / STD |
| 3 | Radius | LR or SR | LR (1.5D) |
| 4 | Angle | 45°, 90°, 180° | 90° |
| 5 | End connection | BW, SW, NPT, flanged | BW |
| 6 | Material and standard | Grade and standard | ASTM A234 WPB |
A complete purchase line reads: Elbow, 90°, LR, BW, NPS 6, SCH 40, ASTM A234 WPB, ASME B16.9, EN 10204 3.1.
Run this pre-order checklist before releasing a PO:
- Confirm the piping class and design code for the line.
- Match elbow schedule to the connecting pipe, not just the nominal size.
- Request mill test certificates with heat numbers traceable to markings.
- Require PMI on all stainless and alloy fittings at receipt.
- Check dimensional tolerances and marking against ASME B16.9 and MSS SP-25.
- Confirm the fitting will pass the project hydrotest pressure.
What Should You Remember When Choosing Elbow Pipe Fittings?
Match angle to the layout, radius to allowable pressure drop, end connection to pipe size and maintenance plan, and material to fluid and environment. Document all six parameters on the purchase order and request certified mill test reports with every shipment.
Understanding elbow pipe fittings types and applications turns selection from guesswork into a repeatable engineering step. Default to long radius, match schedule to pipe, and let the fluid and environment decide the material.
Fitting World Trading LLC supplies carbon and stainless steel pipes, flanges, fittings, and high-pressure fittings from its Dubai showroom to projects across the UAE and GCC.
Need a technical review of your elbow take-off? Contact the FW Trading engineering team for specification support and a fast quote, or message us on WhatsApp.
Frequently Asked Questions
What is the difference between a 90-degree and a 45-degree pipe elbow?
A 90-degree elbow turns flow through a right angle in the shortest distance but adds the most resistance and erosion. A 45-degree elbow turns flow gradually and adds roughly half the resistance, so it suits offsets, steam, and compressed air lines where pressure drop must stay low.
Is a long radius or short radius elbow better for high-pressure lines?
A long radius elbow is better for high-pressure, high-velocity lines because its 1.5D radius lowers pressure drop, turbulence, and outer-wall erosion. Short radius elbows are acceptable only where space is restricted and flow is low, because their 1D radius increases turbulence and local stress. Confirm with the project piping class.
Which stainless steel grade is best for pipe elbows in UAE coastal projects?
SS 316L is the preferred grade for coastal UAE projects because its molybdenum content improves resistance to chloride pitting and crevice corrosion in humid, salt-laden air. SS 304L is adequate for inland, food-grade, and mild chemical service with low chloride exposure. For seawater or high-chloride brine, specify duplex or super duplex stainless steel instead.
Popular Posts
March 22, 2024
March 28, 2024
April 22, 2024
April 30, 2024
